جدول المحتويات
- ما هو التحويل في الغرف النظيفة؟
- Why Medical Devices Need Cleanrooms
- Cleanroom Classes Explained
- The Cleanroom Process
- Medical Applications
- Equipment and Controls
- Cost Considerations
- FAQ
In medical device manufacturing, environmental control is as critical as precision itself. خدمات التحويل في الغرف النظيفة ensure that adhesive components, diagnostic strips, and wearable patches are produced in controlled environments free from particulate contamination. For companies developing medical and healthcare products, choosing a manufacturing partner with certified cleanroom capability is not optional — it is a regulatory and safety necessity. This guide explains what cleanroom converting is, how it works, and what to expect from a qualified cleanroom converting manufacturer.

What Is Cleanroom Converting?
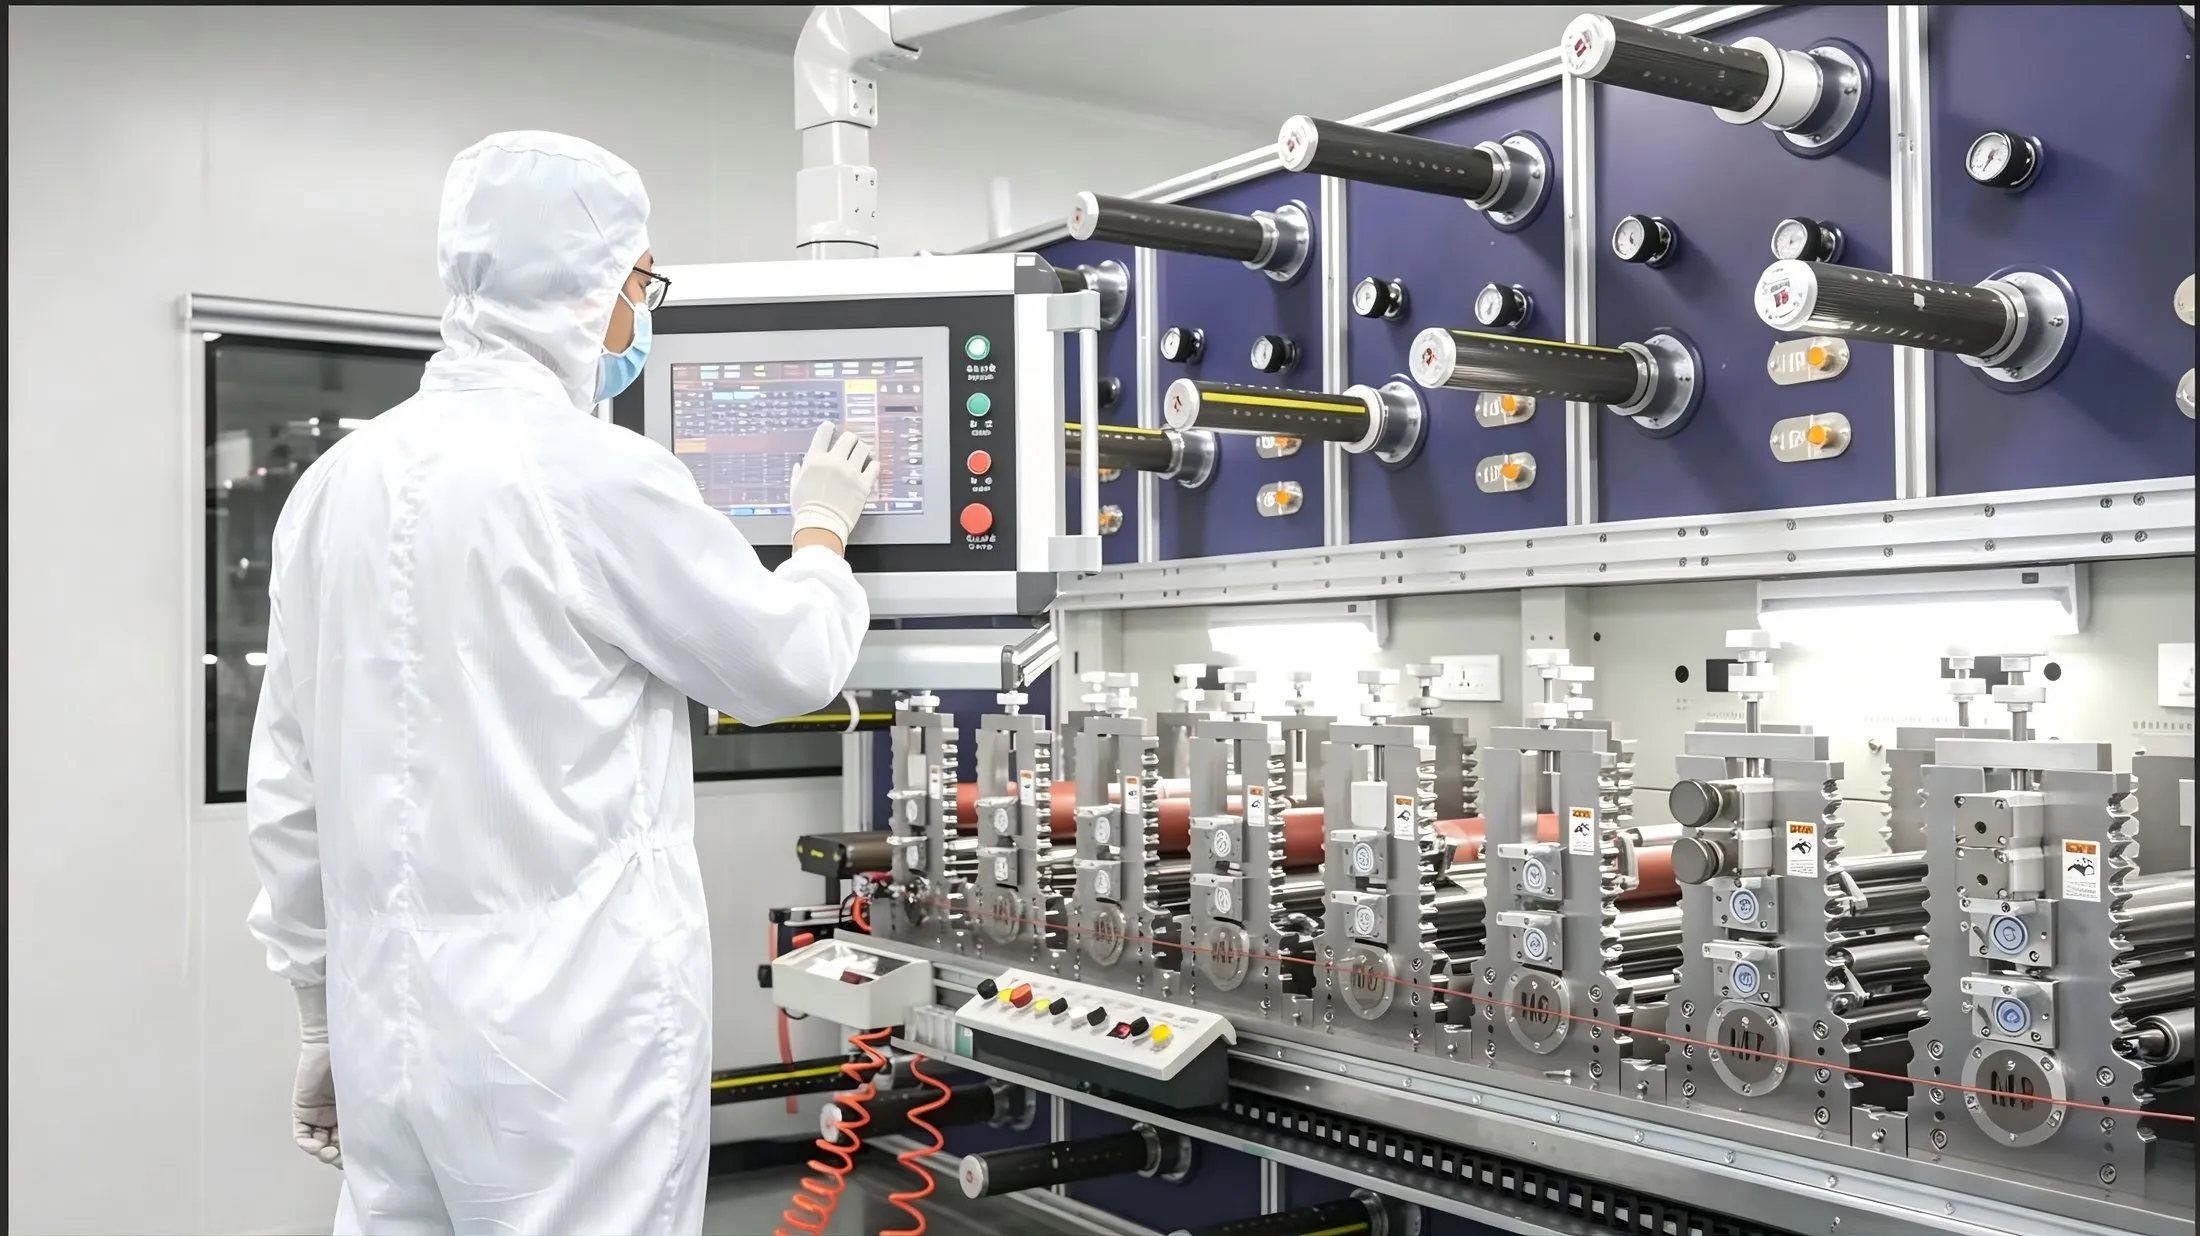
Cleanroom converting is the process of die cutting, laminating, slitting, and finishing medical adhesive materials within an ISO-classified cleanroom environment. Unlike standard industrial die cutting, cleanroom converting controls airborne particulate count, temperature, humidity, and personnel access to meet strict medical device standards. Every step — from material loading to final packaging — occurs within the controlled space.
A qualified cleanroom converting manufacturer combines precision die cutting equipment with controlled environmental conditions. Rotary die cutting presses, laminating machines, and slitting equipment are all housed within the classified cleanroom, not in a standard factory floor. The result is that every component meets bioburden and particulate specifications required for skin-contact and invasive medical devices. Companies looking for medical die cutting services should always verify cleanroom capability before committing to a manufacturing partnership.
Why Medical Devices Require Cleanrooms
Even microscopic particles on a medical adhesive component can cause serious problems:
- Device contamination: Particles can interfere with sensor readings, clog microfluidic channels in diagnostic strips, or cause biofilm formation on implantable components.
- Skin irritation: Particulate residue on adhesive surfaces can cause dermatological reactions, contact dermatitis, or infection in patients with sensitive skin.
- Regulatory non-compliance: Medical devices sold in the US (FDA 21 CFR 820) and EU (MDR 2017/745) require documented controlled production environments. Without cleanroom certification, your device cannot be legally marketed.
- Shelf-life issues: Microbial contamination can accelerate adhesive degradation, promote mold growth, or compromise the sterile barrier during storage.
- Quality inconsistency: Particulate load varies in uncontrolled environments, leading to batch-to-batch variation that is unacceptable in regulated medical products.
Cleanroom Classes Explained
Cleanrooms are classified according to ISO 14644-1 standards. Each class limits the maximum number of particles (0.5 micrometers and larger) per cubic meter of air:
| ISO Class | Particles/m3 | Typical Use | Medical Applications |
|---|---|---|---|
| ISO 5 (Class 100) | 3,520 | Highest level | Implantables, sterile surgical devices |
| ISO 6 (Class 1,000) | 35,200 | High control | Sterile wound care, drug-eluting devices |
| ISO 7 (Class 10,000) | 352,000 | Standard medical | CGM patches, BGM strips, wearable adhesives |
| ISO 8 (Class 100,000) | 3,520,000 | Basic controlled | Non-invasive device components, packaging |
Most wearable medical adhesives and diagnostic components require ISO 7 or ISO 8 cleanroom production. Your device's risk classification and intended use will determine the required class. Learn more about our manufacturing capabilities and cleanroom specifications.
The Cleanroom Converting Process
A professional cleanroom converting operation follows strict protocols at every stage:
- Gowning Protocol: Personnel enter through sequential air locks and wear sterile gowns, hair covers, masks, gloves, and shoe covers.
- Material Entry: Raw materials are wiped down with disinfectant, passed through pass-through chambers, and staged before production.
- Controlled Processing: Die cutting, lamination, and slitting occur within the classified environment. HEPA-filtered air is supplied at 20-60 air changes per hour.
- In-process Monitoring: Airborne particle counters, temperature sensors (20-22 C), and humidity monitors (45-55% RH) are continuously logged.
- Clean Packaging: Finished components are immediately sealed in medical-grade Tyvek or foil pouches within the cleanroom.

Medical Applications That Need Cleanrooms
Several medical product categories specifically require cleanroom converting:
- CGM adhesive patches — direct skin contact for 7-14 days, must be free of microbial contaminants
- BGM test strip components — diagnostic accuracy depends on cleanliness of reaction chambers
- Insulin pump fixation patches — extended wearable device adhesives for subcutaneous insulin delivery
- Wound care dressings — direct wound contact requires sterile or aseptic conditions
- Wearable medical device adhesives — ECG electrodes, EEG pads, continuous monitoring patches
Equipment and Environmental Controls
| Control Type | Specification | Purpose |
|---|---|---|
| HEPA Filtration | 99.97% efficient at 0.3 um | Removes airborne particles |
| Air Change Rate | 20-60 ACH (ISO 7) | Maintains particle count limits |
| Pressure Differential | +10-15 Pa vs adjacent areas | Prevents unfiltered air ingress |
| Temperature | 20-22 C plus/minus 2 C | Stable adhesive performance |
| Humidity | 45-55% RH | Prevents static and material distortion |
| Particle Monitoring | Continuous real-time | Documentation and trend analysis |
Cost Considerations
Cleanroom production carries a cost premium of 10-25% over standard die cutting. This reflects facility investment, gowning procedures, environmental monitoring, and specialized labor. However, for medical devices, this cost is essential for regulatory compliance and product safety. The alternative — contamination-related recalls, regulatory penalties, or patient harm — is far more expensive. When budgeting for medical component development, always include cleanroom production costs in your total cost analysis.
Frequently Asked Questions
What is the difference between a cleanroom and a standard manufacturing floor?
A cleanroom controls airborne particles, temperature, humidity, and air pressure through HEPA filtration and air locks. A standard factory floor has no such controls. For medical devices, cleanroom production ensures consistent bioburden levels and supports regulatory compliance under ISO 13485.
Do all medical adhesive products need cleanroom production?
Most skin-contact and diagnostic components do. Non-invasive, external-facing components may be produced in ISO 8 or standard environments depending on risk classification. Your regulatory strategy determines the required cleanroom class.
How do I verify a manufacturer's cleanroom certification?
Ask for the cleanroom classification certificate, environmental monitoring reports from the last 12 months, and SOPs. ISO 13485 surveillance audits will also verify cleanroom compliance.
Can cleanroom production handle high-volume orders?
Yes. Modern cleanroom converting lines are designed for high-speed rotary die cutting at volumes of millions of pieces per month without quality compromise.
How do I get started with cleanroom converted components?
Contact our engineering team with your component design, material requirements, and volume projections. Visit our contact page to start.
Leetoya provides ISO 7/8 cleanroom converting for CGM patches, BGM components, wearable medical adhesives, and diagnostic strips. Learn more about our cleanroom capabilities or request a quote today.